Production-Integrated & Automated Process Cranes
Process cranes,
built into your line.
Move dies, steel plate and process loads between production stations. Purpose-built lifting attachments and task-specific controls connect the crane to the work on your line.
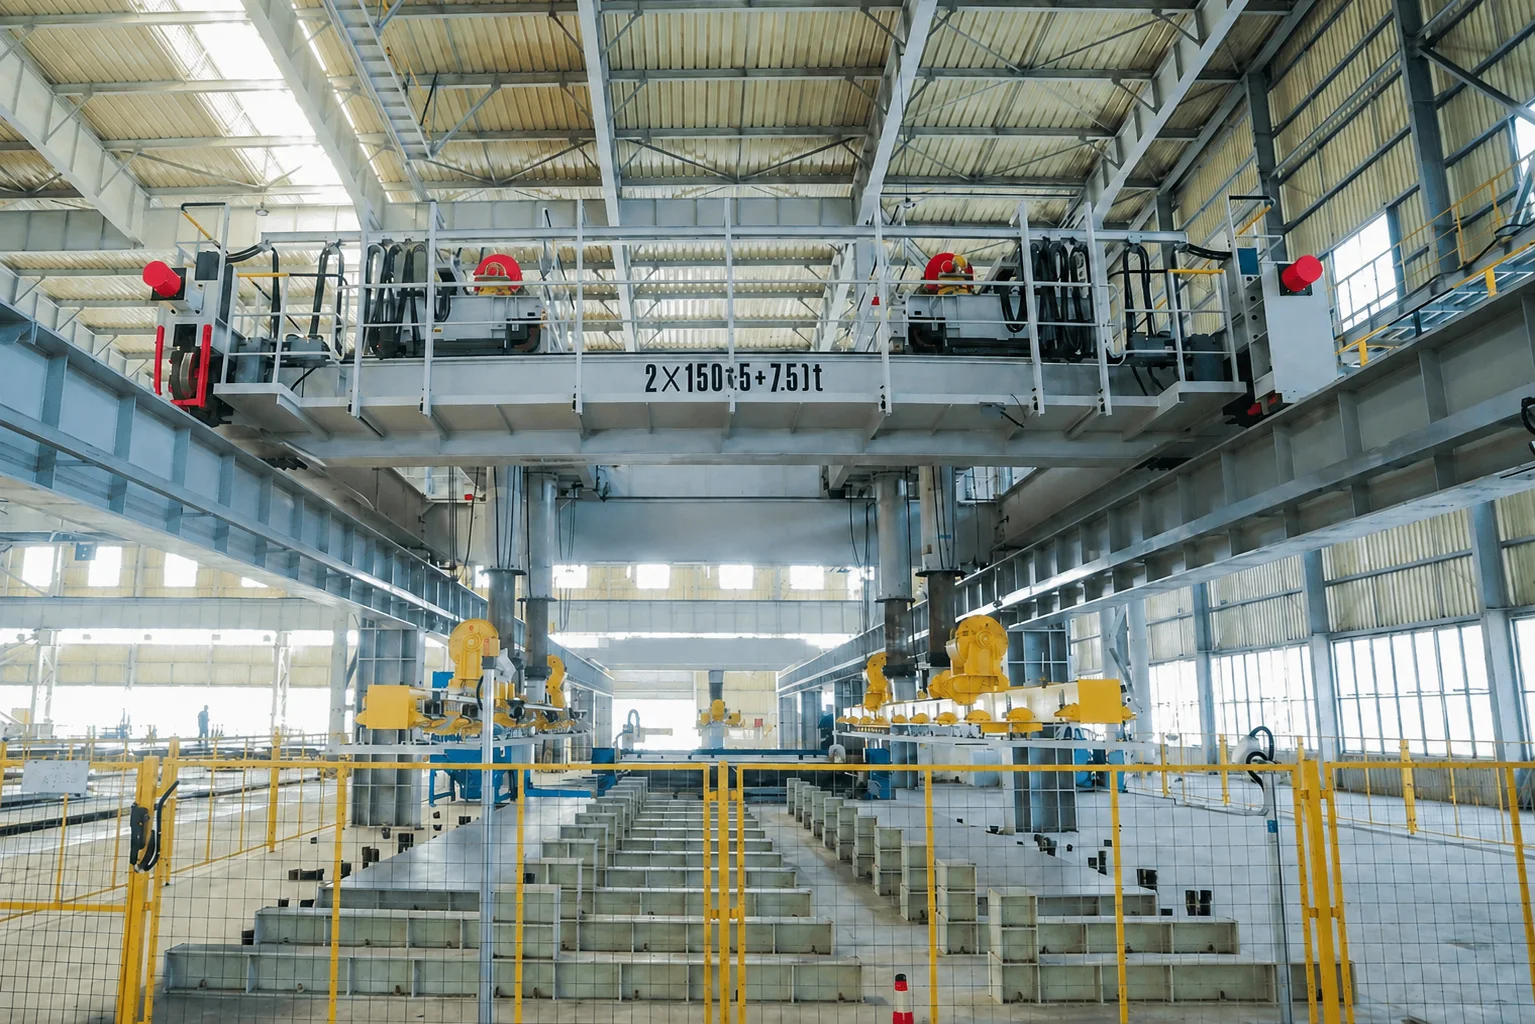
Built around
the load.
From press dies to process materials: the load determines the attachment and the handling arrangement.
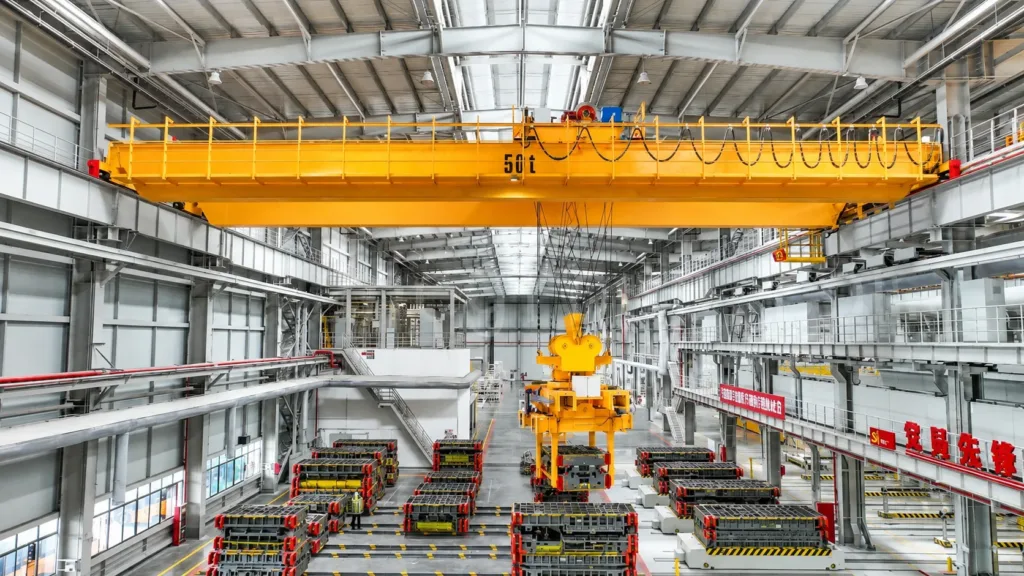
Die handling
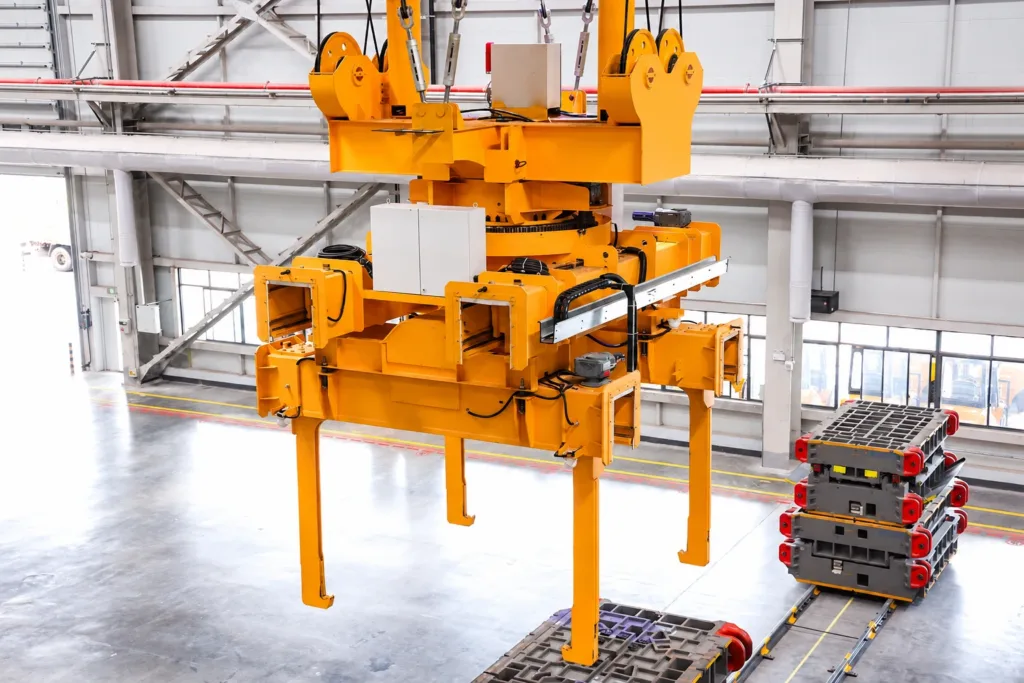
Move dies between storage and press staging positions. Plan around the die range, access to each storage position and the orientation required at the press.
Equipment & operation
- Provide drawings or photos of the die lifting points, the weight and size range, and the required storage and staging positions.
- The crane serves defined storage and staging positions. Clear space around each die matters as much as the travel route above it.
- Positioning assistance can support the operator. Automatic storage transfers additionally need reliable die identification, attachment engagement checks and controlled operating zones.
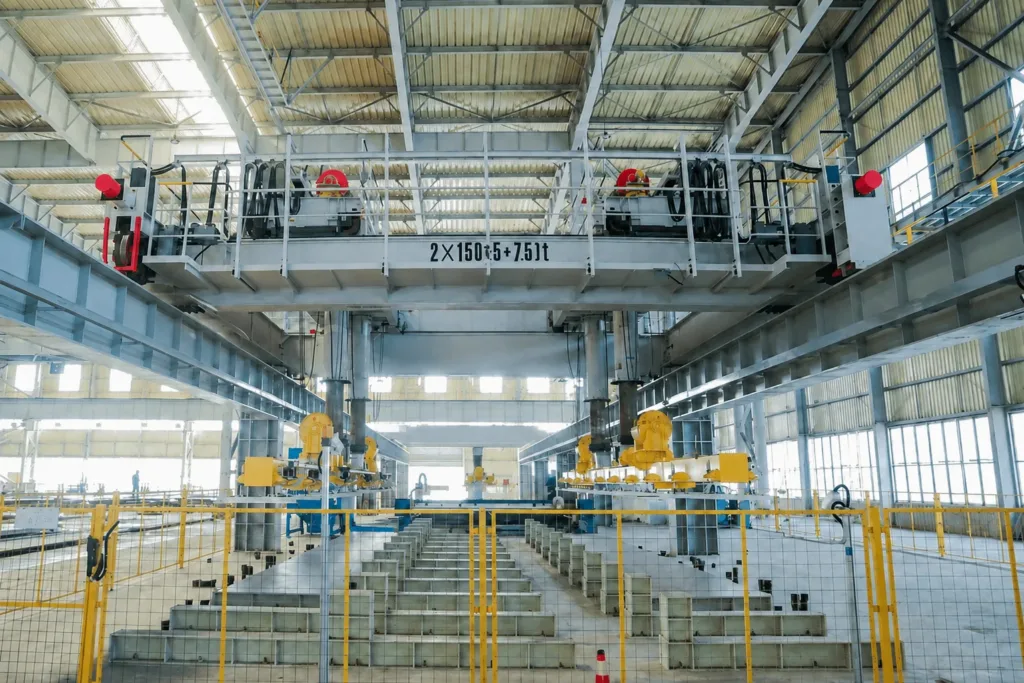
Plate handling
Supply processing equipment and clear cut material. Plate size, thickness and surface determine the lifting method; single-sheet pickup needs a suitable separation and detection system.
Equipment & operation
- Vacuum and magnetic lifting are different configurations. Selection depends on plate material, thickness, surface and whether the task is single-sheet pickup or grouped handling.
- Adjustable vacuum-unit spacing accommodates different plate widths. A combined attachment must keep unused vacuum units clear during magnetic handling.
- The crane can take a positioned plate from the feed equipment and deliver it to the next station. Plate detection, attachment confirmation and the receiving position belong to the transfer design.
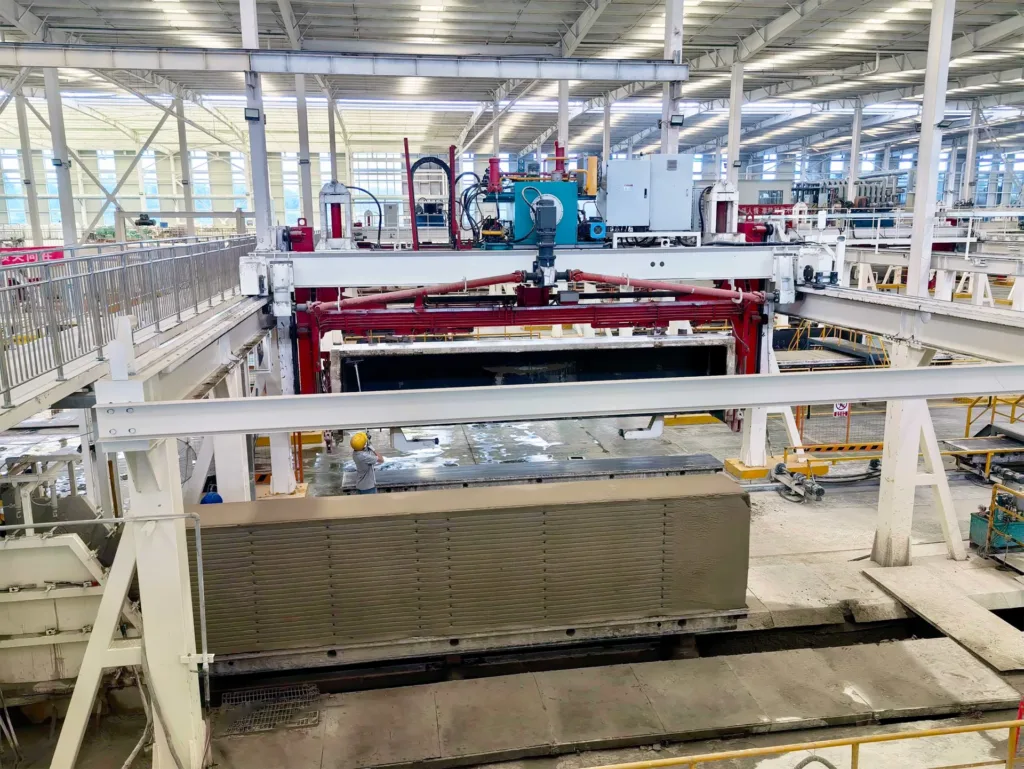
Mould handling
Handle moulds and green bodies through defined production stages. A dedicated lifting frame supports the load in the positions required by the AAC process.
Equipment & operation
- Dedicated lifting devices handle moulds and fragile green bodies. Tilting, opening and demoulding require a frame designed for those actions, not just a suspended hook.
- Some fixed-position AAC designs combine vertical lifting with travel along the line, without a cross-travel trolley. The process layout determines the axes actually needed.
- PLC sequences use position detection to coordinate the lift with the process station. Humidity and heat exposure influence electrical protection and maintenance access; conditions vary by workstation.
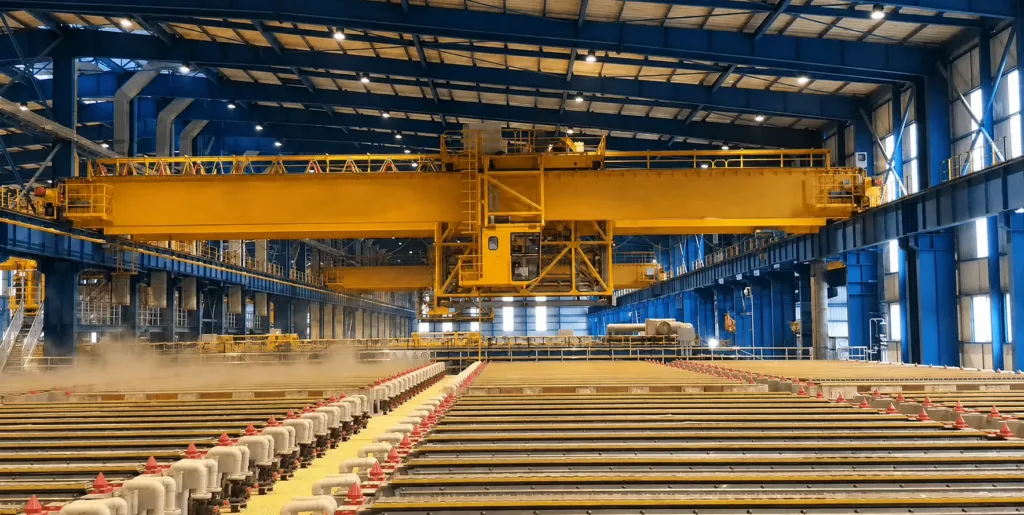
Electrode handling
Lift electrode groups between racks, cells and washing stations. The lifting beam follows electrode spacing; the equipment must suit the wet, corrosive process environment.
Equipment & operation
- Pickup positions follow the electrode group spacing. Guided placement and a drip-collection tray can support transfers from cells to washing equipment.
- Load electrodes from preparation racks into the cells. After processing, remove the relevant electrode group and transfer it to washing, collecting residual electrolyte during the move.
- Positioning aids and automatic sequences are separate from the choice of operator control. Corrosion protection, electrical isolation and the actual cell layout require a defined equipment design.
A closer look.
An adjustable die attachment, shown in detail. Select a numbered feature to explore how it handles different dies.
From plate to process.
A documented steel-plate installation shows how the feed equipment, lifting attachment and crane work together.
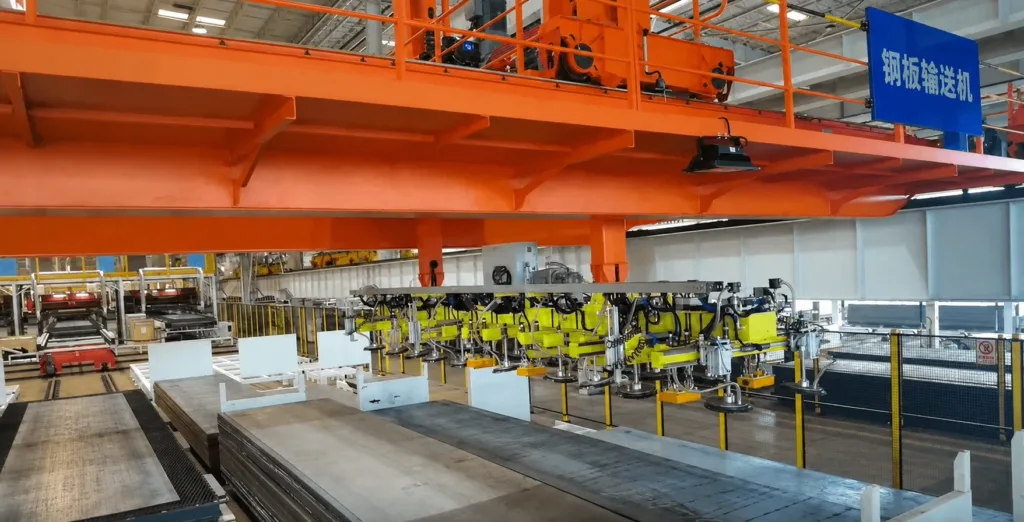
Position. Pick up. Transfer.
The feed platform positions the plate. Vacuum units lift it and mechanical retaining hooks engage underneath. At the receiving station, the crane lowers the plate and releases it for the next operation. This example uses a purpose-built attachment; these functions are not standard on every crane.
Equipment & delivery.
Fissure Tech is your contract partner for the agreed equipment and delivery scope. We coordinate the crane, lifting attachment and controls with your production equipment team.
01Equipment package
We coordinate the crane, dedicated lifting attachment and controls as one package. Manufacturing partners are audited on site before cooperation; the proposal defines the selected equipment and supply scope.
02Installation and commissioning
Installation supervision and commissioning support can be included. The proposal states who handles runway work, erection, power supply and production-machine modifications, so your site team can plan its part.
03Technical handover
The agreed handover includes project drawings, operating and maintenance manuals, and inspection and test records. Factory tests cover equipment functions; site commissioning checks the installed interfaces. Acceptance requirements are defined for the selected equipment.
Common questions.
Existing equipment, station availability and the information needed to begin.
01Can you work with our existing crane?
We first assess its structure, drives, electrics and operating area. That determines whether an upgrade is practical or a dedicated crane is needed.
02What if a receiving station is occupied?
For an automatic system, station-ready signals can hold the transfer until the destination is available. The design also needs an operator recovery mode for interrupted tasks.
03What can we establish in the first discussion?
With your load details and layout, we can discuss suitable lifting arrangements, the level of automation and whether existing equipment may be usable. We then identify the missing information needed to develop a proposal. A complete specification is not required to begin.
Show us the load.
Show us the line.
Send a load photo or drawing and mark the pickup and destination on your layout. We can discuss a suitable handling approach and the site information needed next. If the layout is incomplete, start with what you have.
Discuss your process- Photo or drawing, weight and size range
- Pickup and destination positions
- Required transfers per hour or shift