01 · SOLUTIONS / OPERATING CONTEXTS
The load is only
the start.
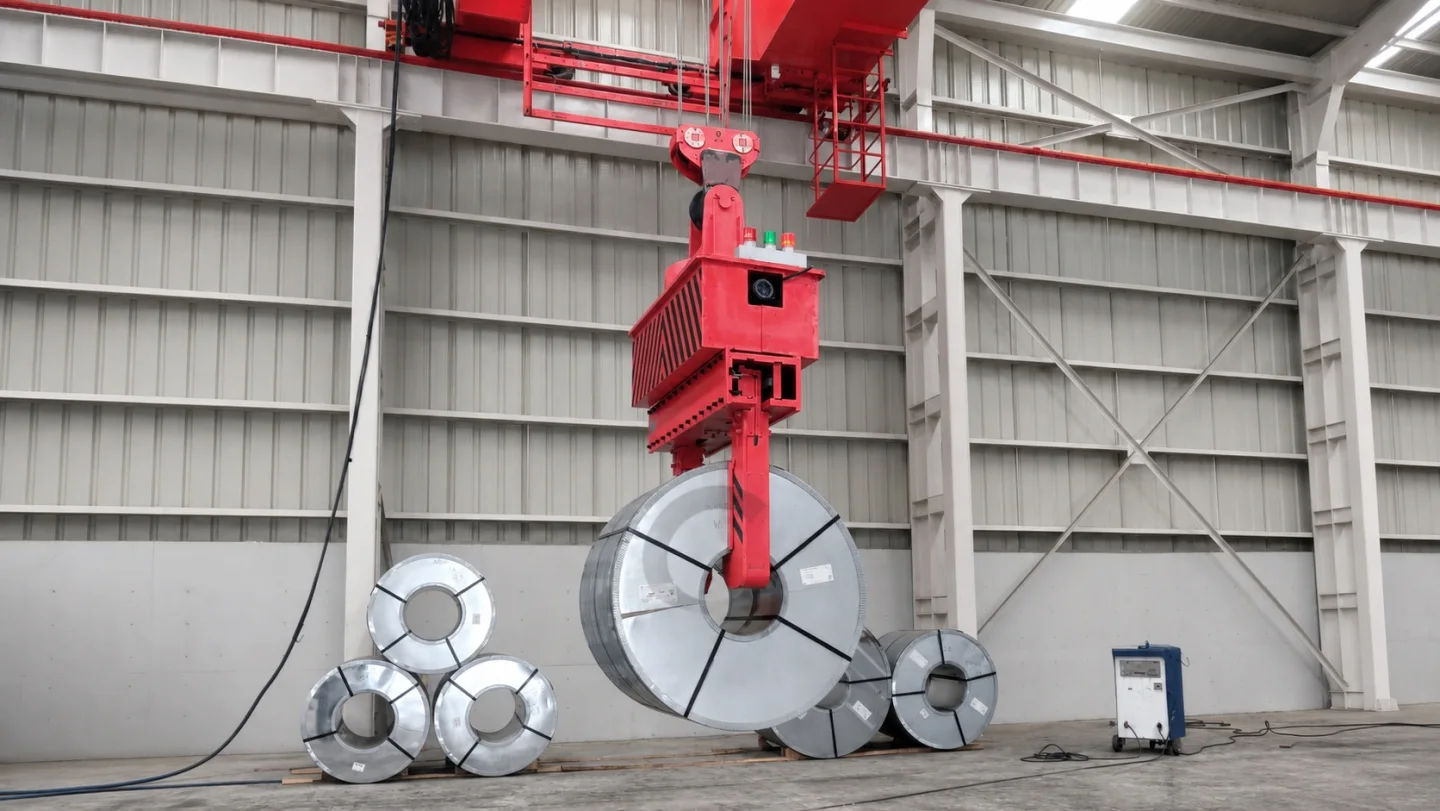
Material handling becomes a production issue when a load crosses a process boundary: receiving into storage, storage into a machine, a hall into a yard, or packing into dispatch. Start with the route. Define the lifting and transfer roles around it.
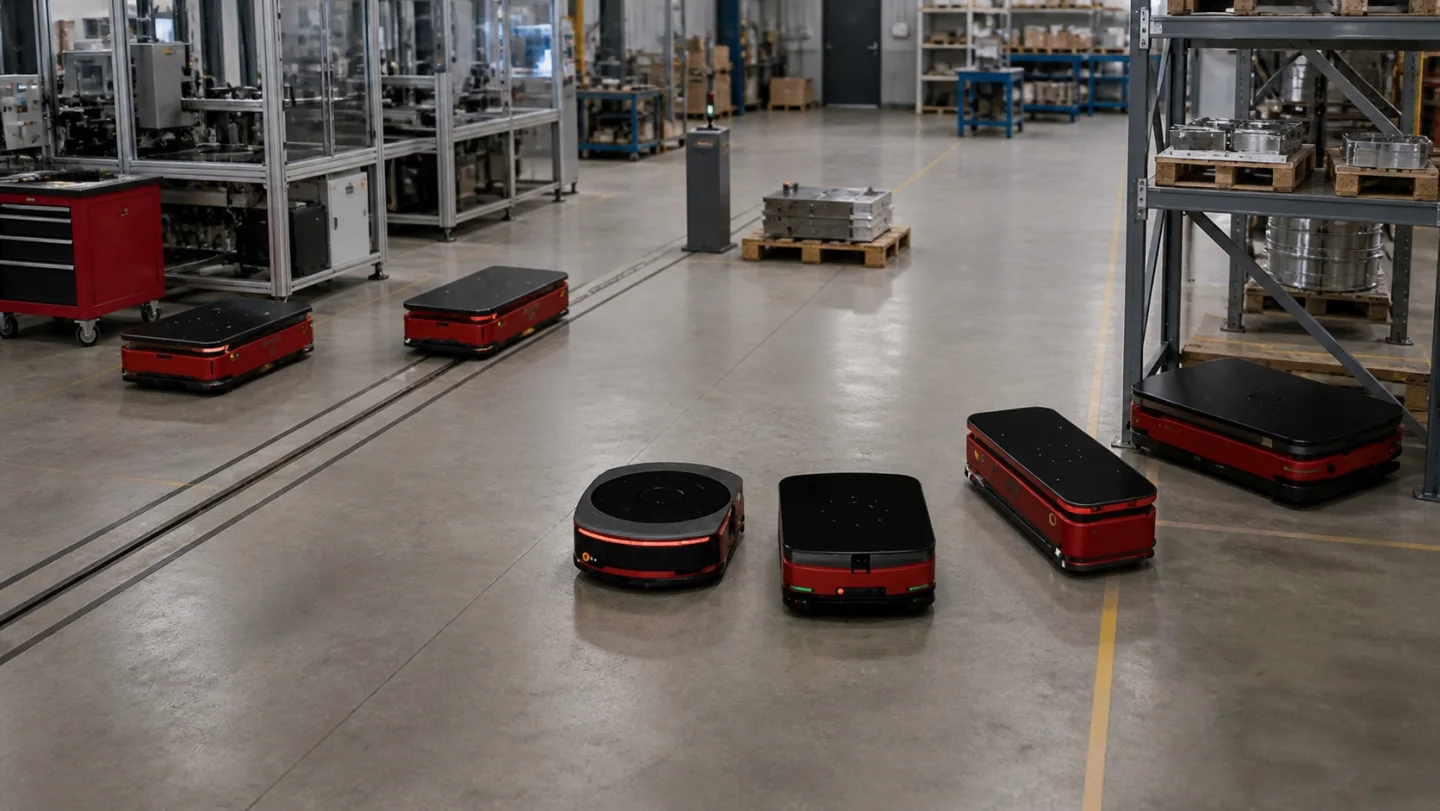
- 01
- 02
- 03
- 04
Start with the operation.
Then define the handling roles.
The product name is not the starting point. The material, hand-offs, operating pressures and system boundary determine which equipment and engineering support belong in the discussion.
- 01
The real material.
Define the load form, condition, attachment and any change between receiving and dispatch.
- 02
Every hand-off.
Mark where the load waits, changes equipment, crosses traffic or enters another process zone.
- 03
The operating pressure.
Heat, cold, dust, wind, hygiene, timing, access and redundancy can change the handling concept.
- 04
The system role.
Separate equipment, structure, controls, interfaces, recovery and acceptance before defining supply scope.
Where does the flow
break down?
Each industry has its own material, timing, access and hand-off conditions. Select one to inspect the process moments that define the handling discussion.
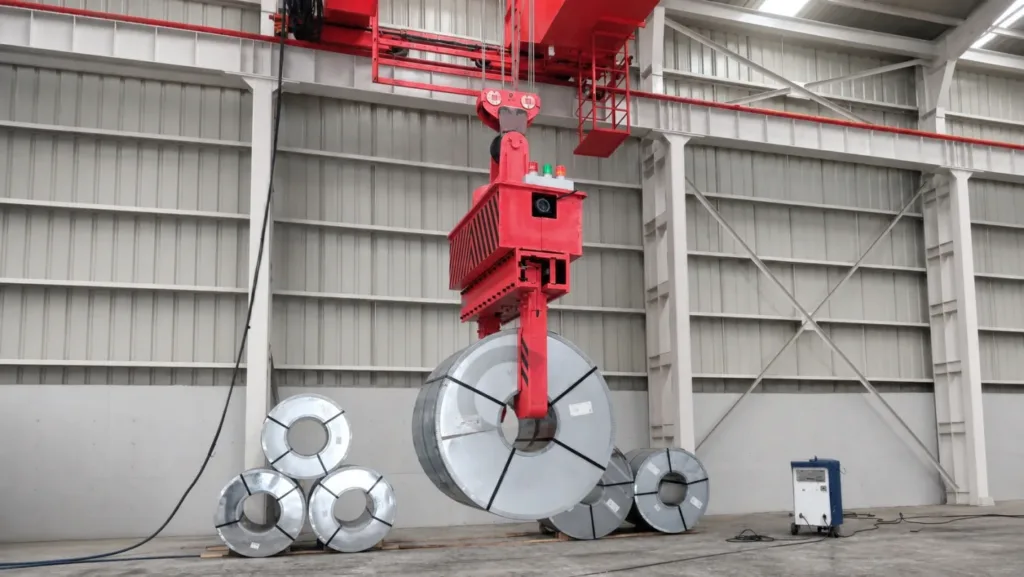 Steel Mills & Metal ProcessingReceiving, processing, inter-bay transfer and dispatch all change how coils, plate and long products should move.
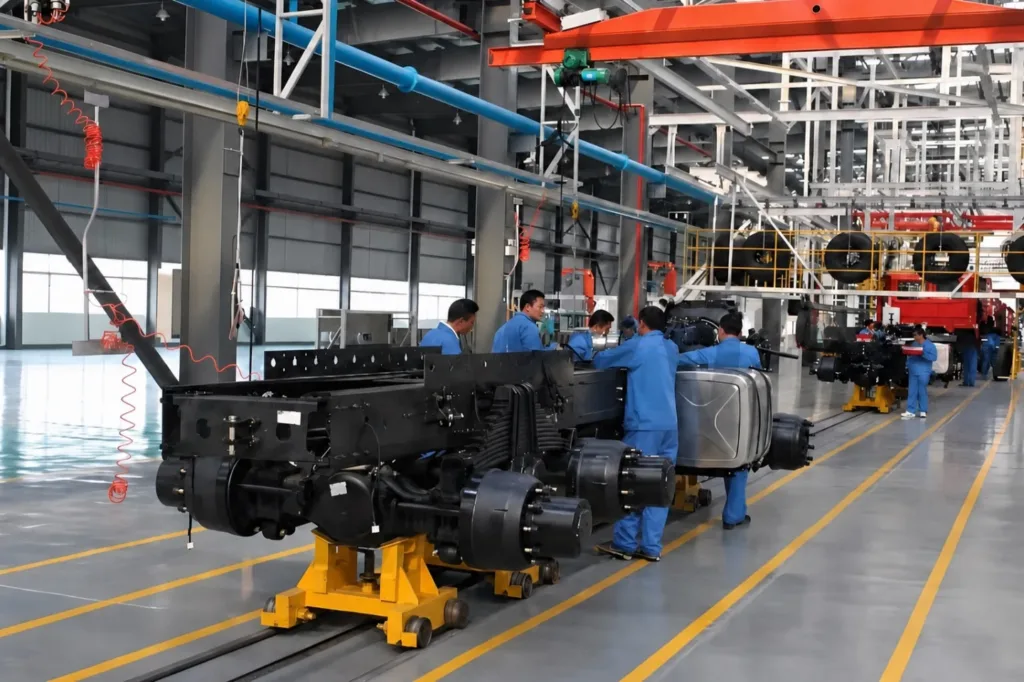 Automotive & Assembly ManufacturingTool readiness, line-side presentation, inter-zone hand-offs and maintenance access decide whether flow keeps pace.
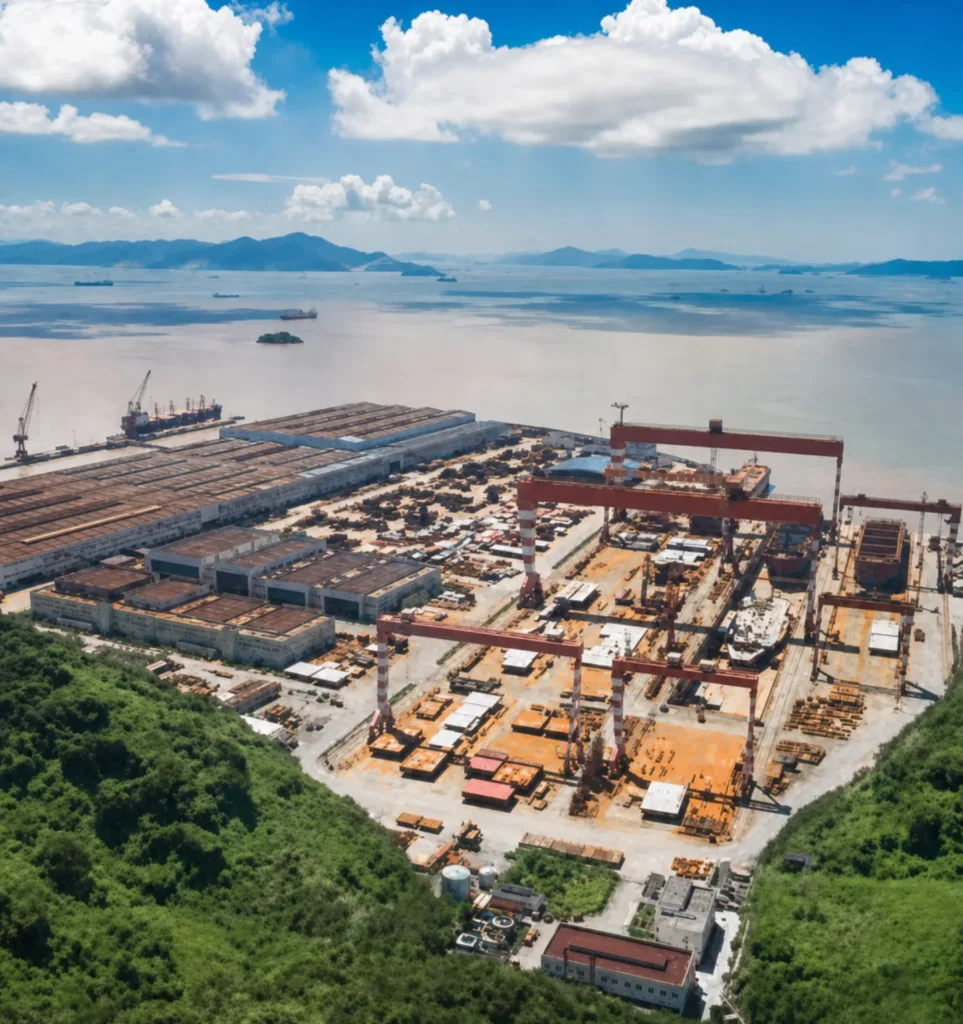 Shipyards & Marine FabricationPlate fabrication, block assembly, hall-to-yard transfer and outfitting each create a different movement boundary.
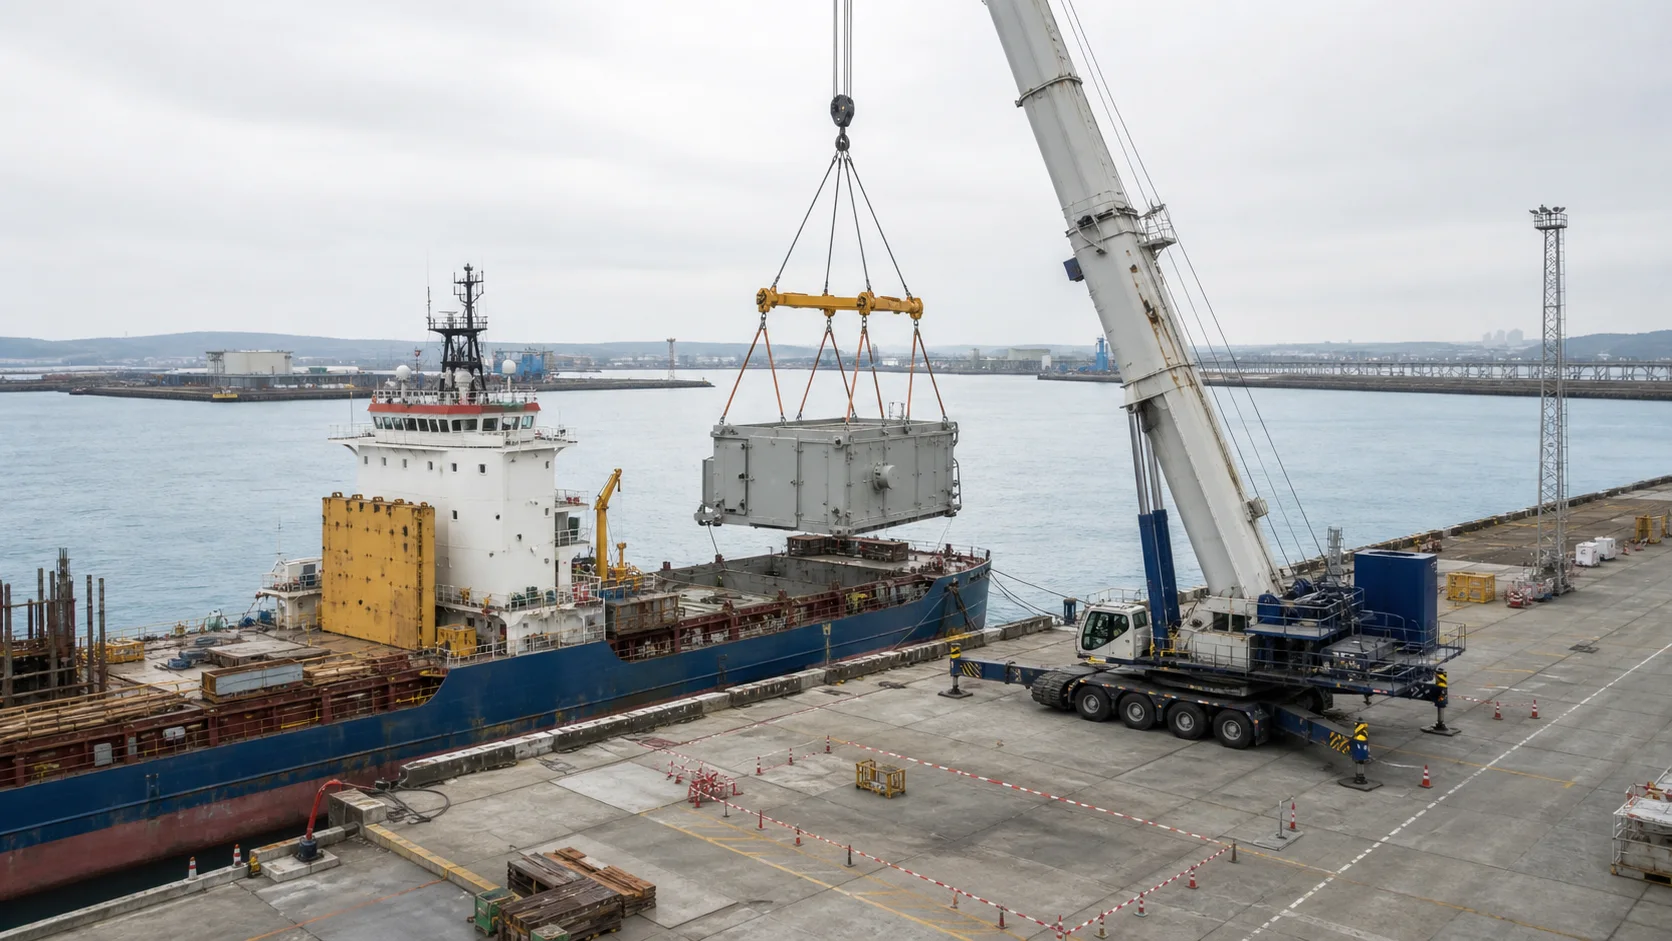
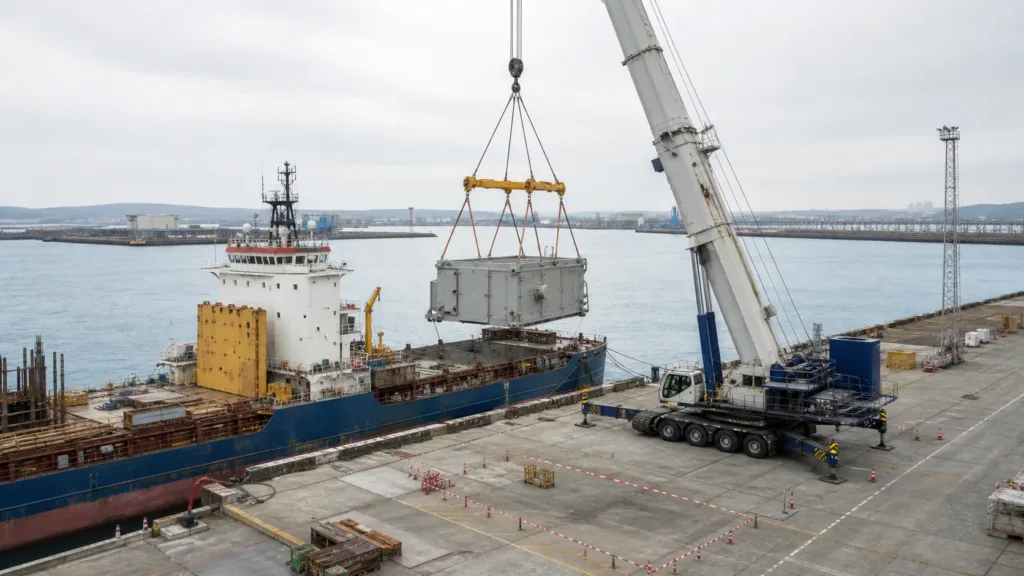 Ports & Marine TerminalsVessel interface, quay transfer, yard storage and landside hand-off define whether each cargo stream can move safely and predictably.
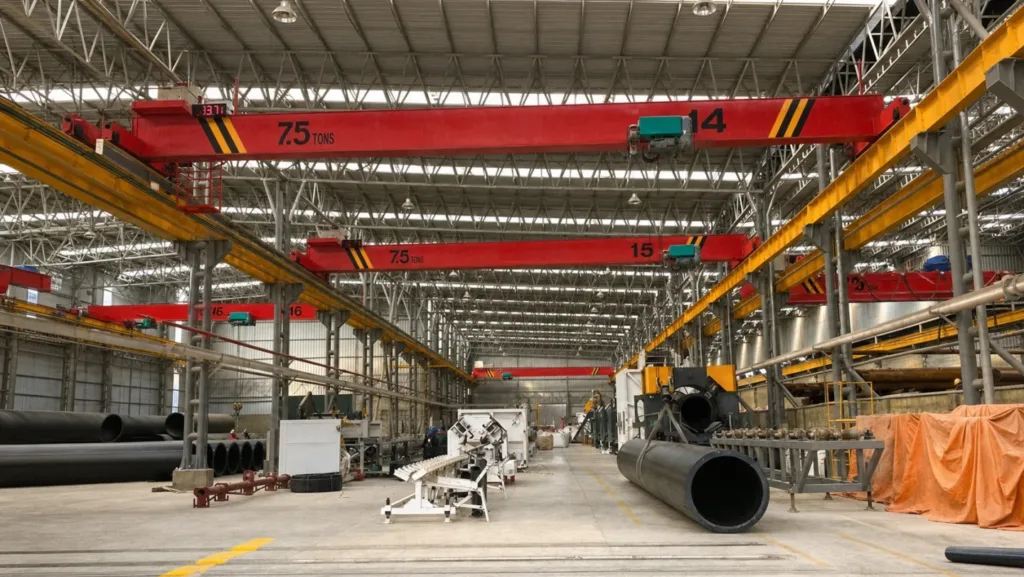 Machinery Manufacturing & Service WorkshopsReceiving, machine service, precision assembly and repair routes make access and positioning as important as lift.
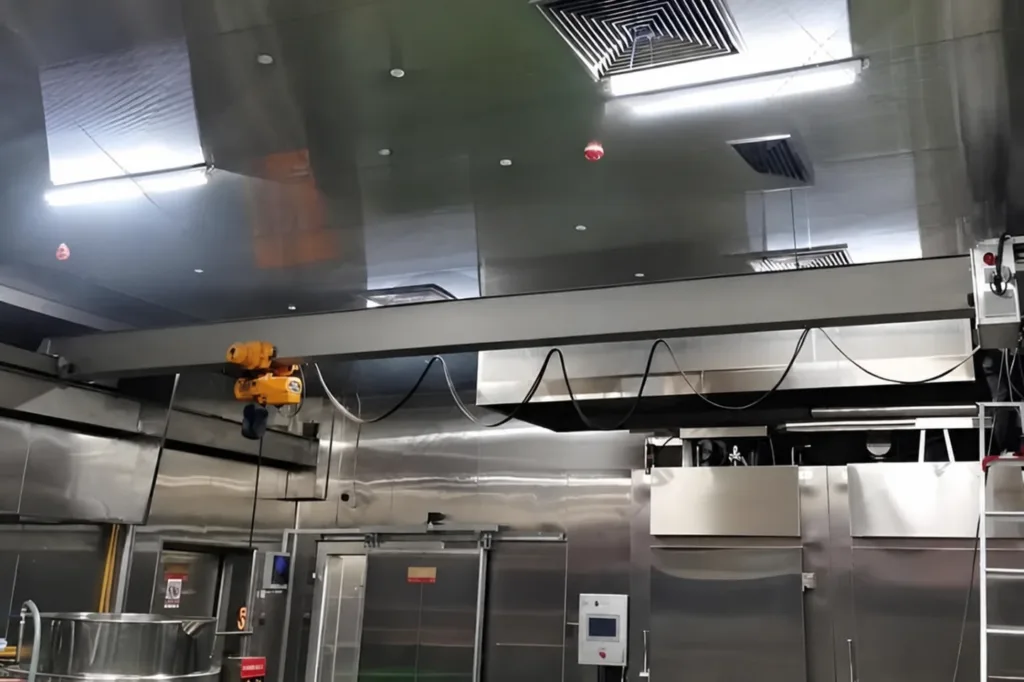 Food & Beverage ProcessingMaterial condition, cleaning access, short maintenance windows and packed-product flow shape the work.
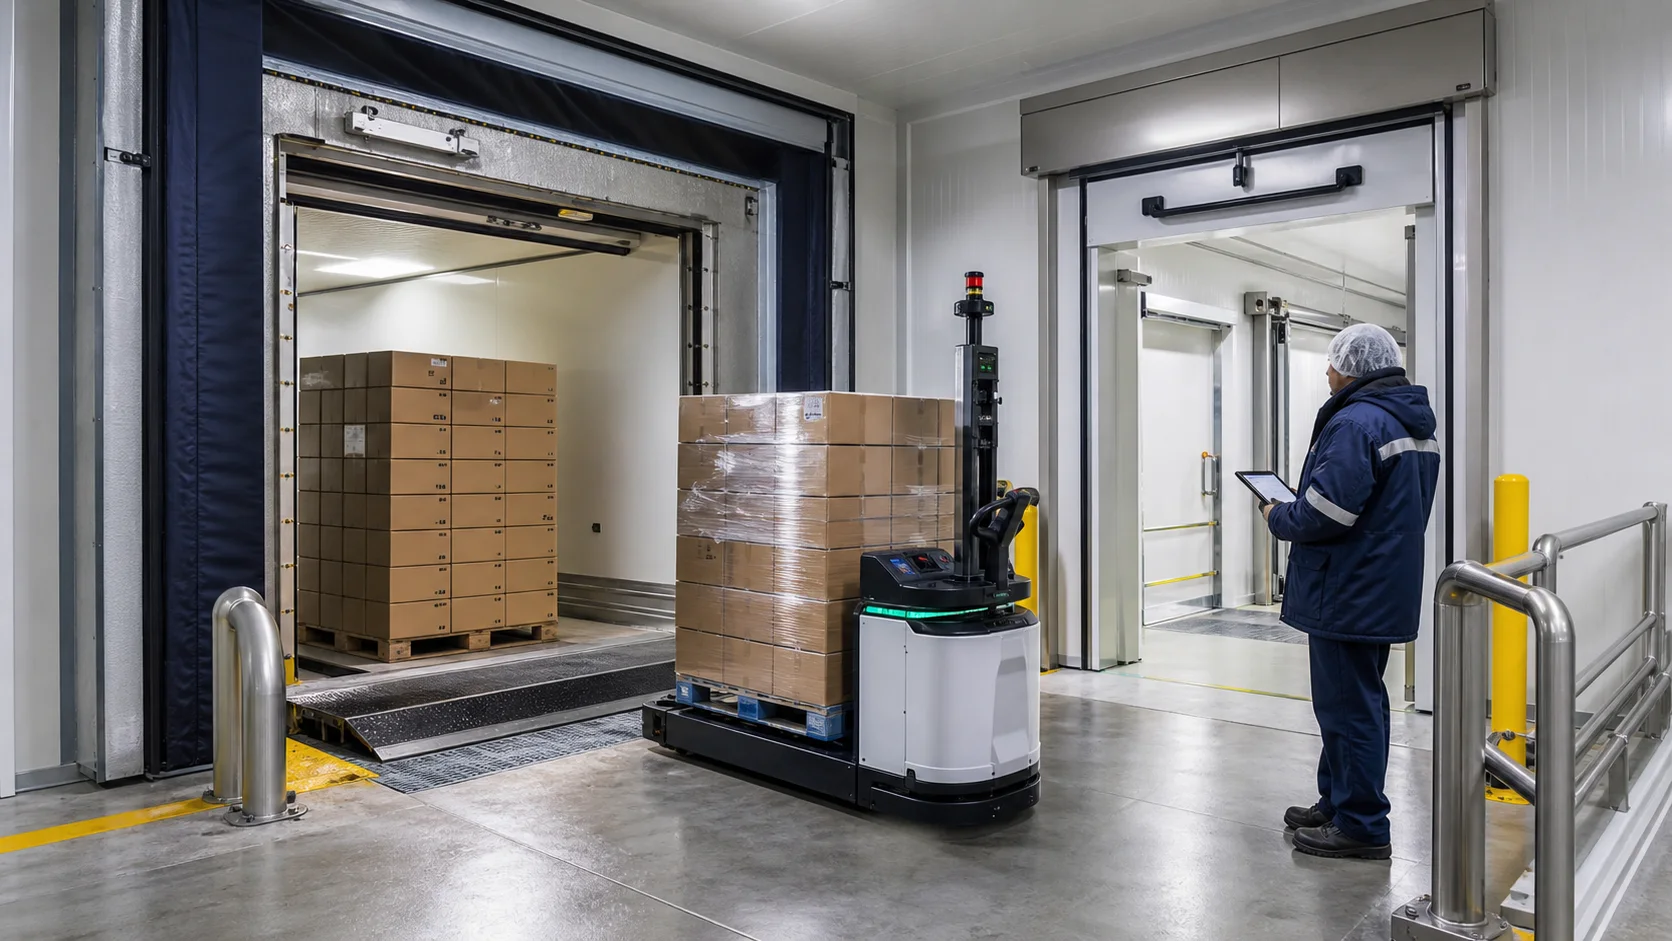
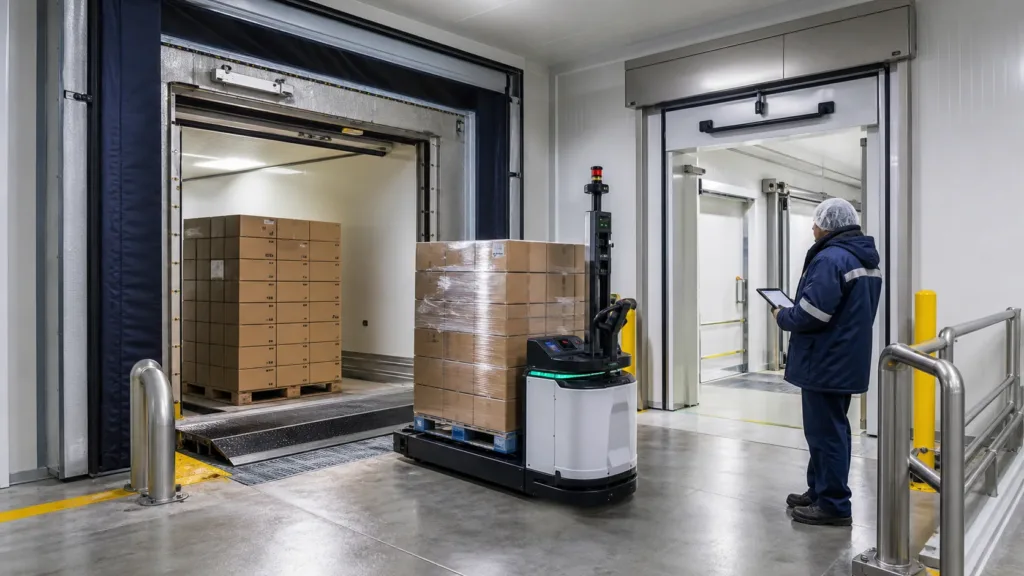 Cold-Chain Storage & DistributionTemperature-controlled receiving, zone transfer, storage and dispatch must preserve product condition without exposing people or flow to avoidable delay.
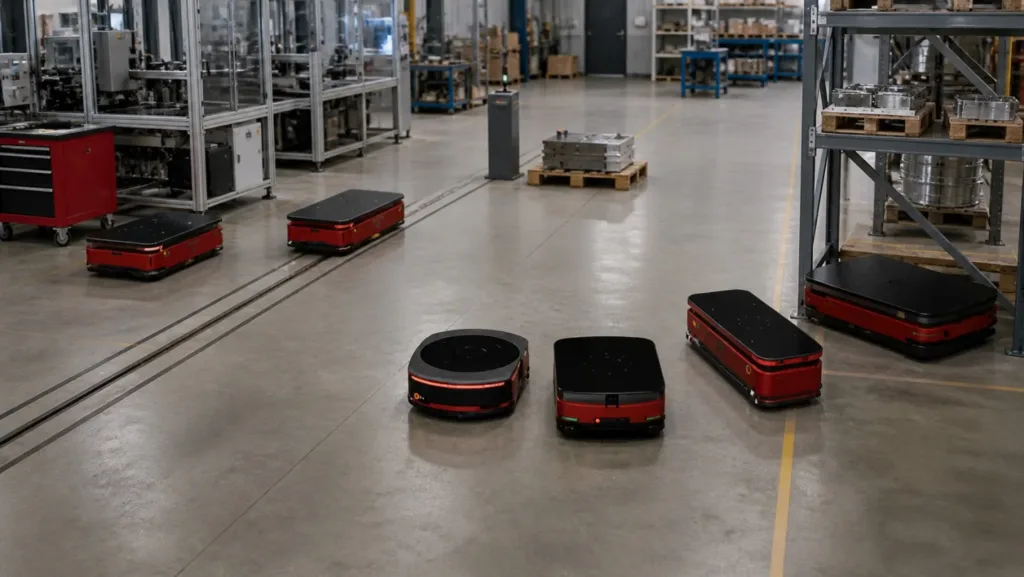 Warehousing, Distribution & IntralogisticsInbound verification, replenishment, consolidation and dock hand-off determine whether inventory moves predictably.
FOLLOW THE MATERIAL, NOT THE MACHINE.
Material condition, process rhythm and the next hand-off define the handling concept from incoming stock to finished dispatch.
START WITH THE LOAD'S FIRST WAITING POINT.
Incoming coil, plate, bar or billet must leave transport, be identified and enter a stable staging pattern without blocking inspection or the next unload. The handling question is not only weight: it is whether the material must be turned, protected, held by a specific attachment, or queued by grade and next operation.
Discuss receive & stage- Coil / plate / bar / billet
- Vehicle → inspection → staging
- Attachment, traceability & storage access
- Load form and dimensions
- Packaging and pick points
- Vehicle interface
- Inspection access
- Staging density
- Material identification
Receiving and staging coverage; attachment and anti-sway discussion; a defined transfer route between the arrival point and the next bay.
KEEP THE MACHINE SERVED, NOT SURROUNDED.
At cutting, forming, rolling, machining or fabrication stations, material must arrive in the correct sequence and leave before the work area becomes storage. The concept is shaped by cycle rhythm, approach direction, operator clearance and how the load is presented to the machine during changeover.
Discuss feed the process- Semi-finished steel / mill rolls
- Staging → process station → buffer
- Cycle timing & machine interface
- Cycle and changeover pattern
- Machine loading geometry
- Surface or heat condition
- Set-down tolerance
- Shared aisle conflicts
- Buffer quantity
Bridge coverage across process bays, local handling at machine interfaces and a longitudinal transfer route where the bays do not connect.
MAKE THE HAND-OFF VISIBLE BEFORE IT BECOMES A BOTTLENECK.
Semi-finished material often crosses between process bays. The decisive issue is the route: does it cross people, forklifts, doors, furnaces, rail lines or an existing crane boundary? This is a route problem first, and only then a question of equipment.
Discuss cross bays- Plate / sections / coil / assemblies
- Process bay → transfer corridor → next bay
- Cross-traffic & fixed boundaries
- Origin and destination
- Route length
- Cross-traffic
- Floor or rail condition
- Hand-off time
- Maintenance fallback
Transfer-cart or RGV corridor, coordinated coverage between bays, or a modernisation discussion where the existing route is fixed.
HOLD THE RIGHT FINISHED LOAD WITHOUT RE-SHUFFLING THE YARD.
Finished coil, plate, section or fabricated packages need accessible storage that protects dispatch order. Density alone is not the objective: the right load must leave without repeated reshuffles while packing, trucks and people keep a clear working route.
Discuss dispatch- Finished coil / plate / section
- Finish → storage → loading
- Sequence, access & truck hand-off
- Dispatch sequence
- Storage rule
- Packaging condition
- Truck interface
- Dwell time
- Pedestrian separation
Dispatch-side coverage, defined storage access and a controls/visibility discussion for route and status confirmation.
WHY THIS INDUSTRY NEEDS ITS OWN HANDLING LOGIC.
Steel handling changes as the material changes. Incoming coils, plate, billets and long products arrive with transport packaging and inspection requirements; semi-finished material must then meet the rhythm and geometry of cutting, rolling, forming or fabrication; finished material must remain accessible in the right dispatch sequence.
A useful concept therefore maps the complete route: where the load waits, how it is attached, which boundaries it crosses, how people and vehicles share the bay, and what happens when one process or crane is unavailable. Heat, dust, vibration and repetitive cycles may further change components, controls and maintenance access.
- 01
CHANGING LOAD CONDITION
Coils, plate, billets, rolls and fabricated assemblies cannot be treated as one generic load.
- 02
PROCESS CONTINUITY
Receiving, production feed and dispatch need different buffers so one delay does not occupy the next work zone.
- 03
HARSH OPERATING CONTEXT
Heat, dust, vibration, surface protection and attachment method can change the entire equipment brief.
Four moments.
One material flow.
Use the route below as a first technical map. Each moment changes what needs to be measured, protected, timed or handed over.
START WITH THE LOAD'S FIRST WAITING POINT.
Incoming coil, plate, bar or billet must leave transport, be identified and enter a stable staging pattern without blocking inspection or the next unload. The handling question is not only weight: it is whether the material must be turned, protected, held by a specific attachment, or queued by grade and next operation.
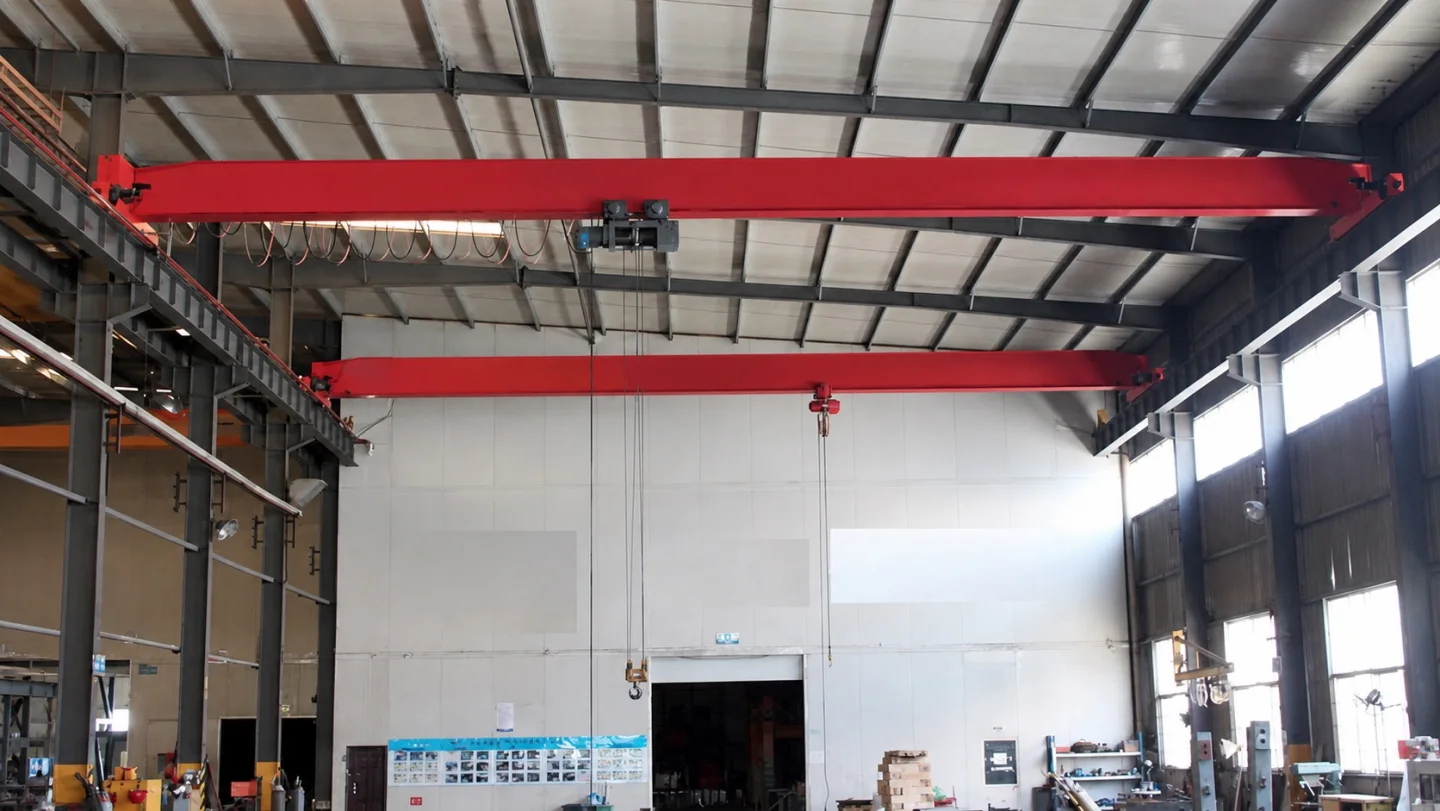
KEEP THE MACHINE SERVED, NOT SURROUNDED.
At cutting, forming, rolling, machining or fabrication stations, material must arrive in the correct sequence and leave before the work area becomes storage. The concept is shaped by cycle rhythm, approach direction, operator clearance and how the load is presented to the machine during changeover.
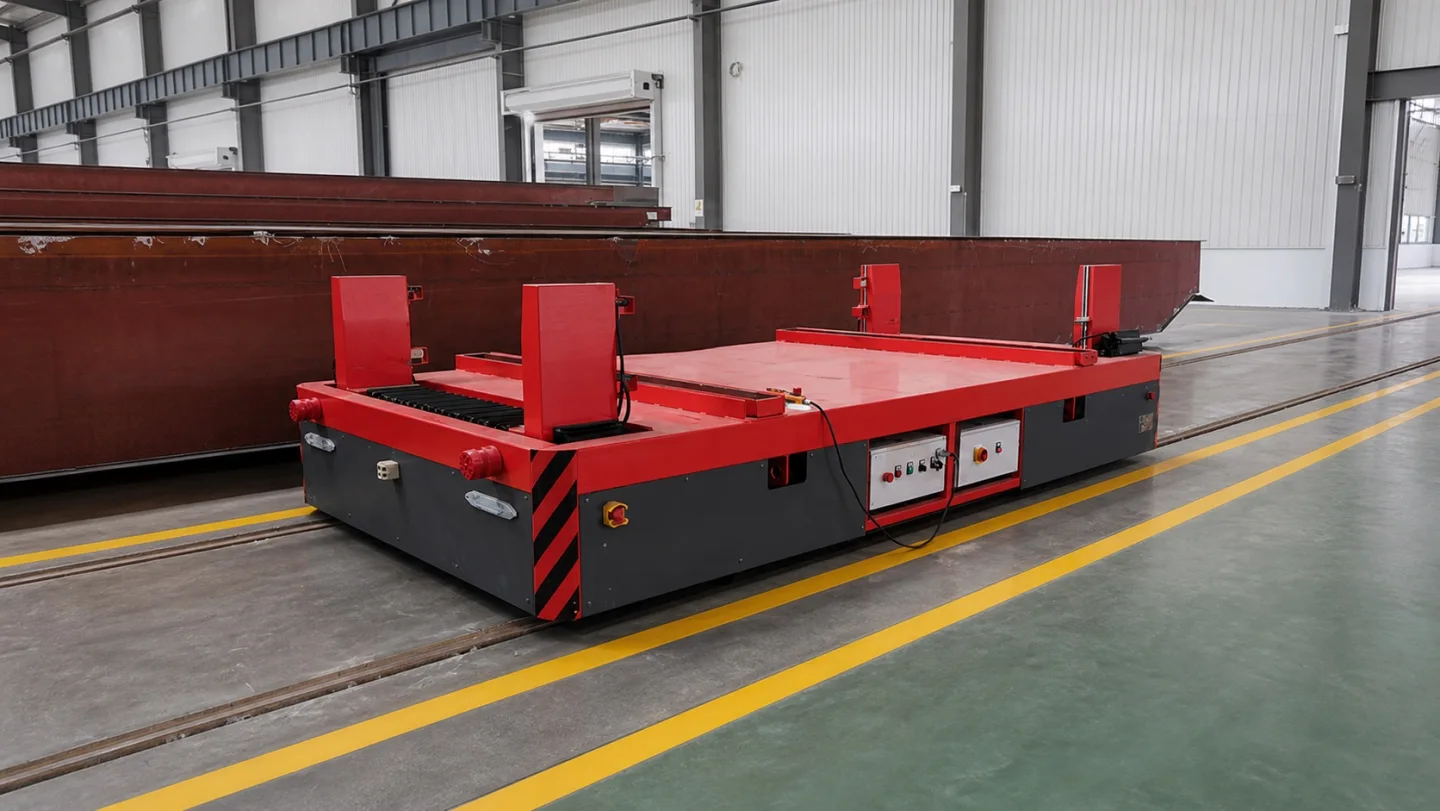
MAKE THE HAND-OFF VISIBLE BEFORE IT BECOMES A BOTTLENECK.
Semi-finished material often crosses between process bays. The decisive issue is the route: does it cross people, forklifts, doors, furnaces, rail lines or an existing crane boundary? This is a route problem first, and only then a question of equipment.
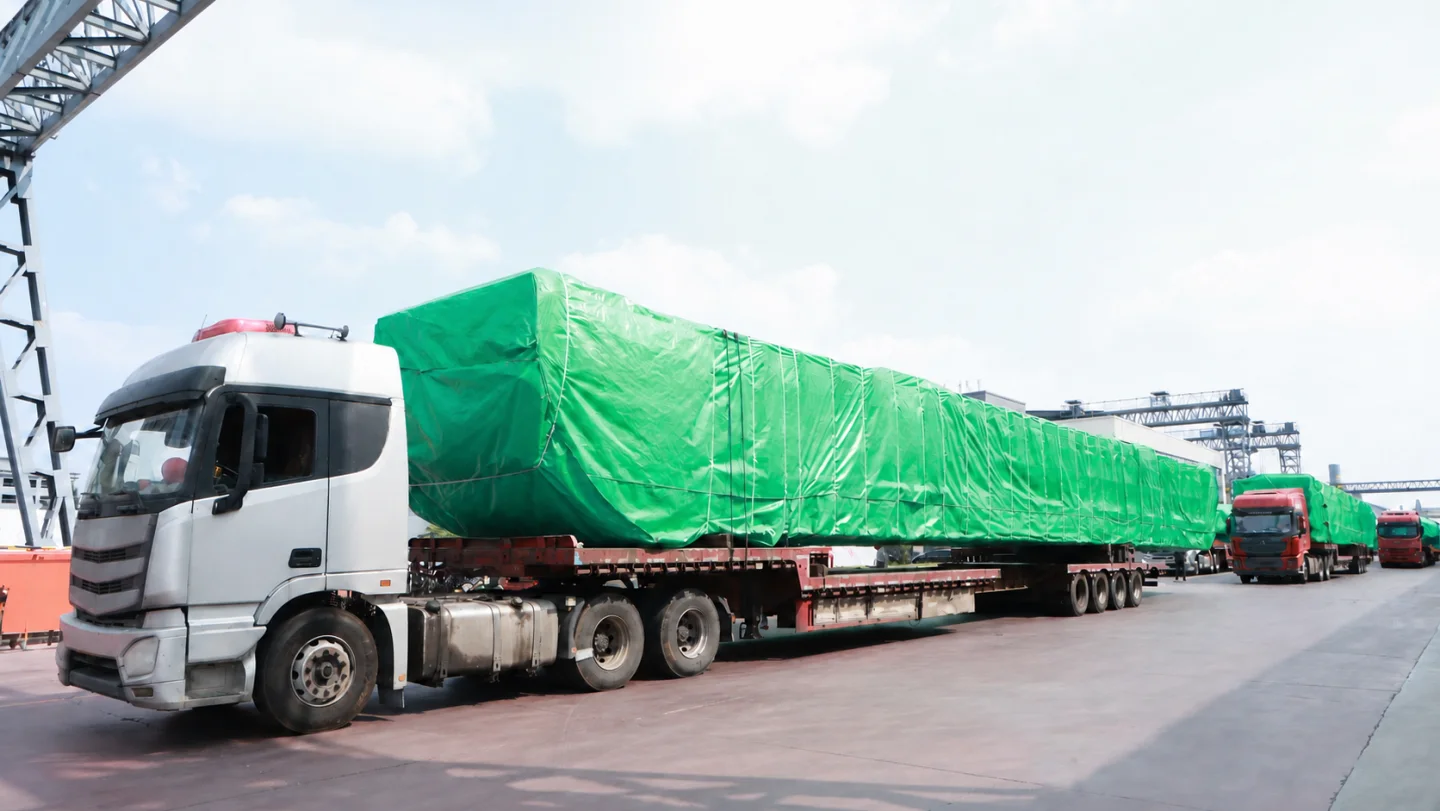
HOLD THE RIGHT FINISHED LOAD WITHOUT RE-SHUFFLING THE YARD.
Finished coil, plate, section or fabricated packages need accessible storage that protects dispatch order. Density alone is not the objective: the right load must leave without repeated reshuffles while packing, trucks and people keep a clear working route.
What changes
the concept?
- A
ATTACHMENT STRATEGY
Define pick points, load stability, surface sensitivity and whether turning or controlled orientation is required.
- B
DUTY AND CYCLE
Use the real movement frequency, loaded travel and waiting pattern rather than average daily tonnage.
- C
BAY AND ROUTE BOUNDARY
Identify doors, rail lines, traffic crossings and the exact hand-off between lifting or transfer systems.
- D
RECOVERY AND MAINTENANCE
Plan how production continues when a route, attachment or crane is under inspection or unavailable.
Choose the equipment.
Then add the operating constraint.
Explosion protection, cleanliness, electrical insulation, availability, heat and automation can change components, controls, verification and acceptance across more than one product family. Treat these as project requirements, not as separate equipment categories.
Explosion-Protected Lifting
Classified gas or dust zone, group and temperature classChanges permitted motors, brakes, enclosures, wiring, controls, documentation and acceptance evidence.Define this requirement02Clean & Controlled Environment Handling
Cleanliness class, particle limits, material and lubrication restrictionsChanges exposed surfaces, materials, lubrication, enclosure, cleaning access and contamination controls.Define this requirement03Electrically Insulated Lifting
Voltage context, required insulation points and contact riskChanges the insulation architecture, monitoring, component separation and configuration-specific verification.Define this requirement04High-Availability & Redundant Lifting
Failure consequence, required recovery time and maintenance accessChanges drive and brake architecture, fallback states, maintainability and proof of continued availability.Define this requirement05High-Temperature & Molten-Material Handling
Molten or high-temperature load, radiant heat and personnel exposureChanges shielding, cabling, control position, emergency strategy and protection of critical components.Define this requirement06Automation, Remote & Unmanned Operation
Remote or unmanned cycles, system hand-offs and fault recoveryChanges sensing, interlocks, permissions, recovery logic, interfaces and responsibility boundaries.Define this requirementBring the route,
not a perfect spec.
A layout, route sketch, load list, photos or process sequence is enough to begin. The first discussion identifies the operating boundaries, missing inputs and handling roles worth evaluating.
MAP YOUR HANDLING ROUTE- Form, dimensions, condition, attachment and stability
- Origins, destinations, waiting points, doors and crossings
- Sequence, buffer, cycle, peak flow and recovery
- Structure, floor, access, temperature, dust, hygiene or wind
- Signals, traffic, responsibility, verification and delivery boundary