Process & Specialised Cranes · Product family
Map process.
Control risk.
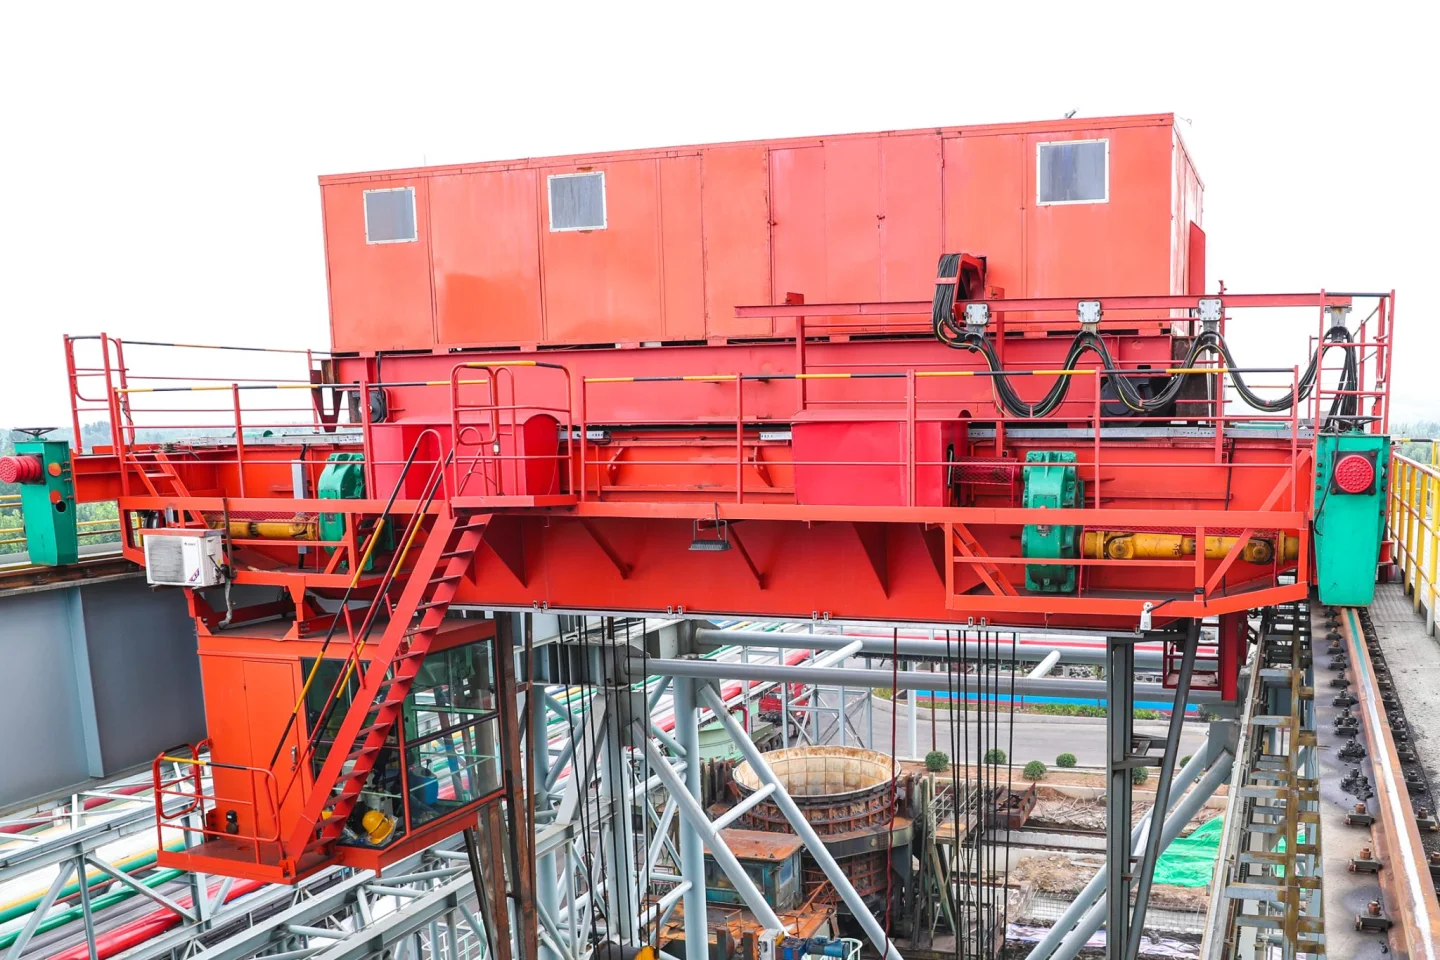
When the crane becomes part of production, the load state, operating sequence, availability and failure consequence define the system before bridge geometry or nominal capacity.
- 01
- 02
- 03
- 04
- 05
Six crane families.
One equipment tree.
Start with the load or production job the buyer can recognise. Add the special operating requirement after choosing the crane family, so the same crane is not duplicated under competing categories.
Metals & Foundry Crane Systems
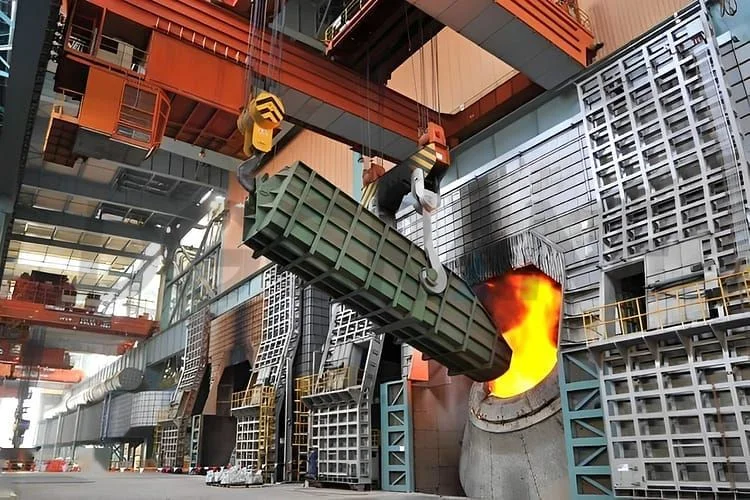
Charging, casting, ladle, forging and quenching crane systems for metals processes.
- Charging, ladle, casting, forging and quenching
- Molten or hot-load containment and heat protection
- Production duty, redundancy and recovery
Metal Stock Handling Cranes
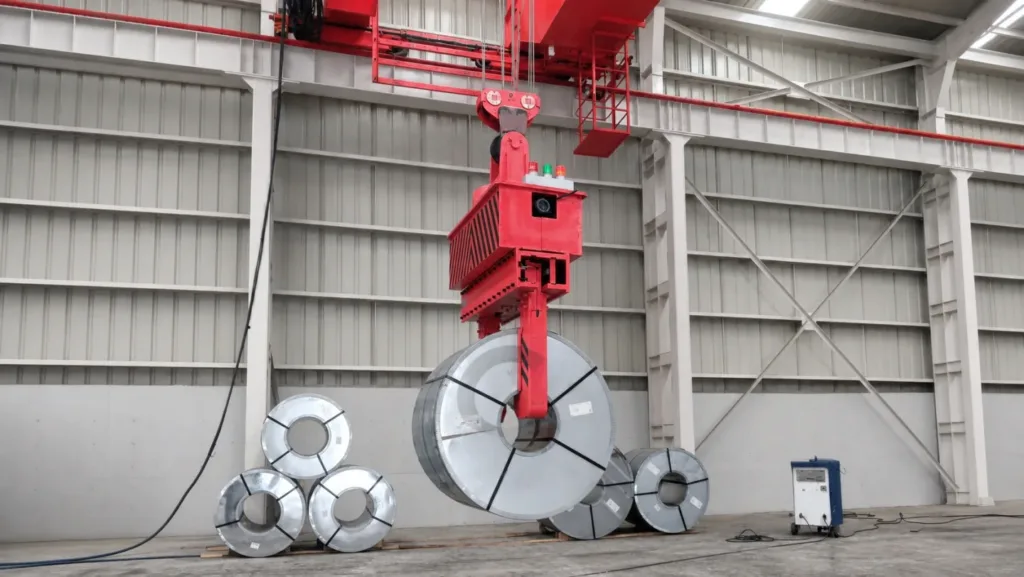
Cranes for slabs, billets, coils, plate, rolls, scrap and magnetic handling routes.
- Slabs, billets, coils, plate, rolls and scrap
- Magnet, clamp, beam and C-hook engagement
- Storage, traceability and dispatch flow
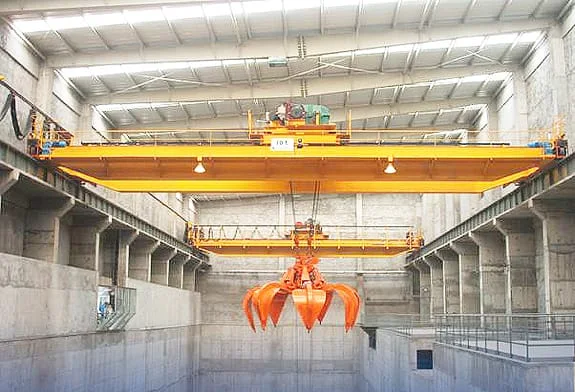
Waste, Biomass & Bulk Process Cranes
Grab and automated feed systems for waste bunkers, biomass, sludge, slag and loose bulk.
- Waste, biomass, sludge, slag and loose bulk
- Receive, blend, reclaim and furnace-feed cycles
- Manual, semi-automatic or unmanned operation
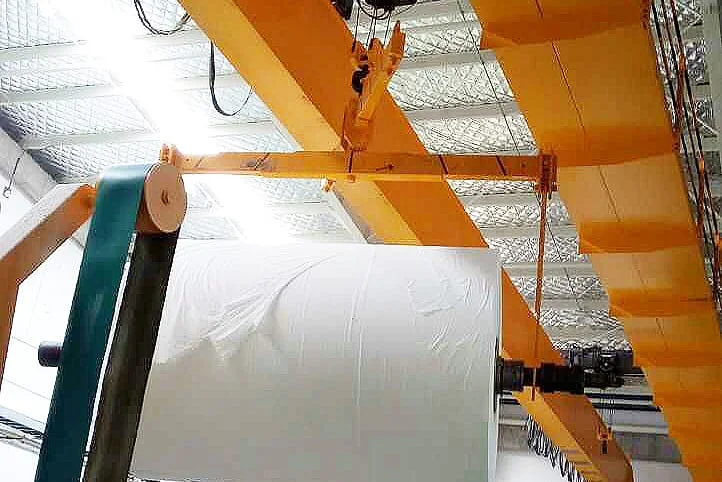
Paper, Roll & Woodyard Crane Systems
Roll, paper-machine maintenance and woodyard handling systems subject to evidence and media review.
- Paper-machine reel and roll handling
- Automated roll stores and gentle engagement
- Pulp, timber feed and woodyard routes
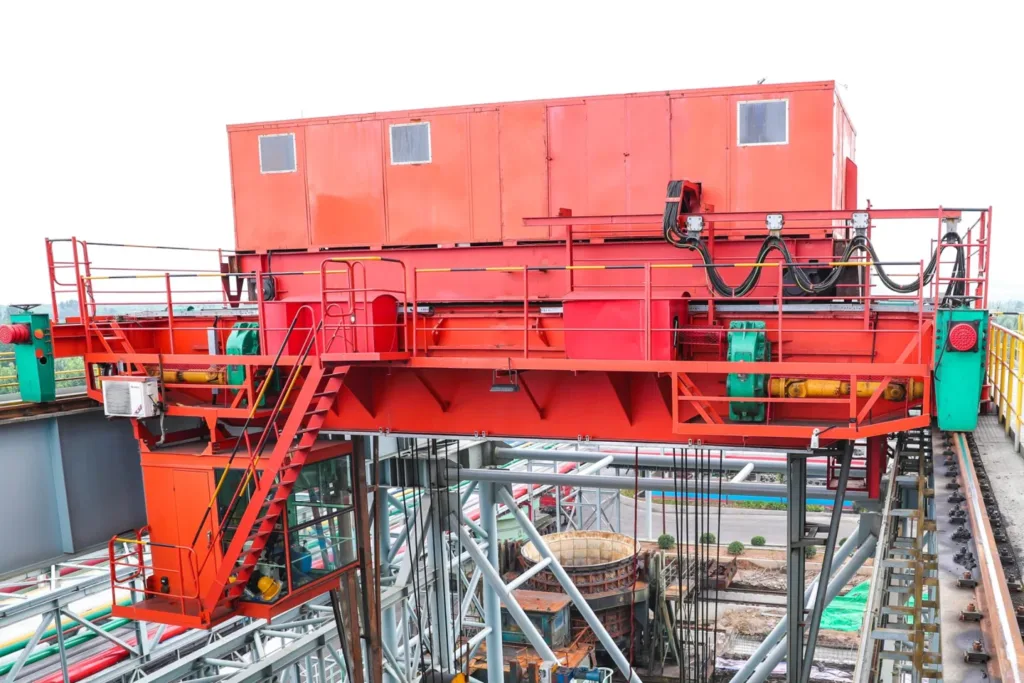
Production-Integrated & Automated Process Cranes
High-cycle, synchronised, multi-trolley and automated cranes integrated with production equipment.
- Machine, press, tool and vessel service
- Multi-trolley, synchronised and turning tasks
- Process signals, interlocks and degraded modes
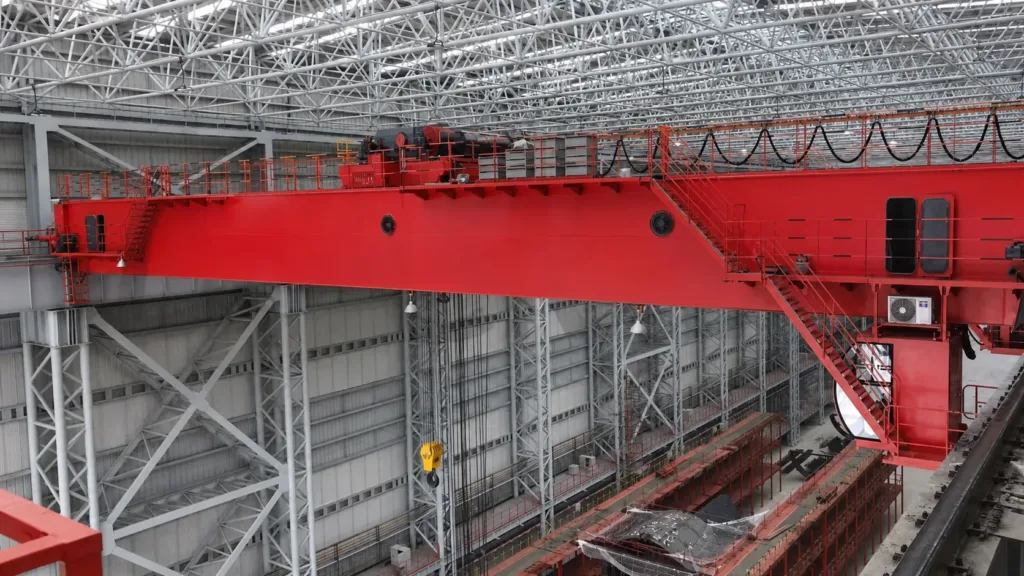
Energy & Critical-Maintenance Crane Systems
Power, hydropower and critical-maintenance lifting systems with project-specific evidence gates.
- Turbine, generator and plant-component handling
- Hydropower gates and maintenance lifting
- Erection, outage and long-idle readiness
Compare the operating regime.
Not catalogue dimensions.
This matrix separates unlike process-crane families without pretending one specification table can size every specialised crane.
Keep the product.
Add the constraint.
Explosion protection, cleanliness, insulation, redundancy, heat and automation change engineering and proof across more than one product family. They remain Solution requirements—not another six competing crane categories.
- 01
Explosion-Protected Lifting
Zone, gas or dust group, temperature class and equipment scope must be defined before selection.
Add this requirement to the brief - 02
Clean & Controlled Environment Handling
Cleanliness, material, lubrication, particle and access requirements define the handling system.
Add this requirement to the brief - 03
Electrically Insulated Lifting
Insulation points, voltage context, monitoring and equipment evidence are configuration-specific.
Add this requirement to the brief - 04
High-Availability & Redundant Lifting
Failure modes, recovery time and maintenance access determine redundancy and availability architecture.
Add this requirement to the brief - 05
High-Temperature & Molten-Material Handling
Heat, splash, load state, emergency strategy and personnel exposure govern the lifting design.
Add this requirement to the brief - 06
Automation, Remote & Unmanned Operation
Operating sequence, sensing, recovery, interfaces and responsibility boundaries define automation scope.
Add this requirement to the brief
Three connected decisions.
One production boundary.
The sequence accumulates project evidence. It does not send the buyer around the same page or pretend each stage is another product category.
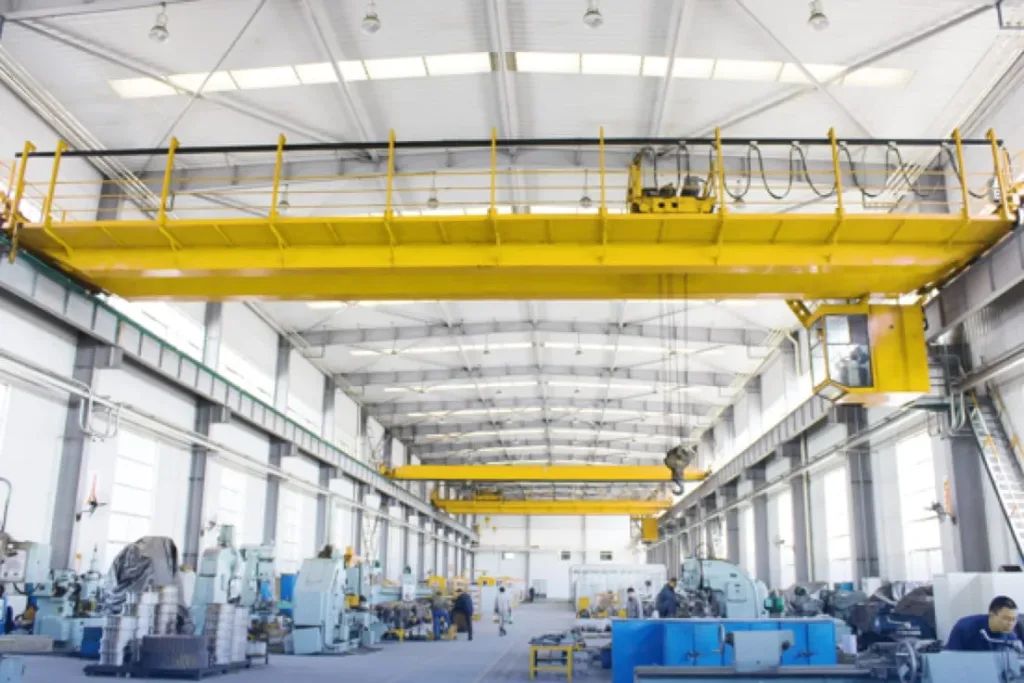
Describe the load as it changes through the process. 01What is being moved—and how must it be engaged at each hand-off?
Mass alone is not enough. Temperature, shape, centre of gravity, stability, surface, containment and release method define the attachment and the credible motion path.
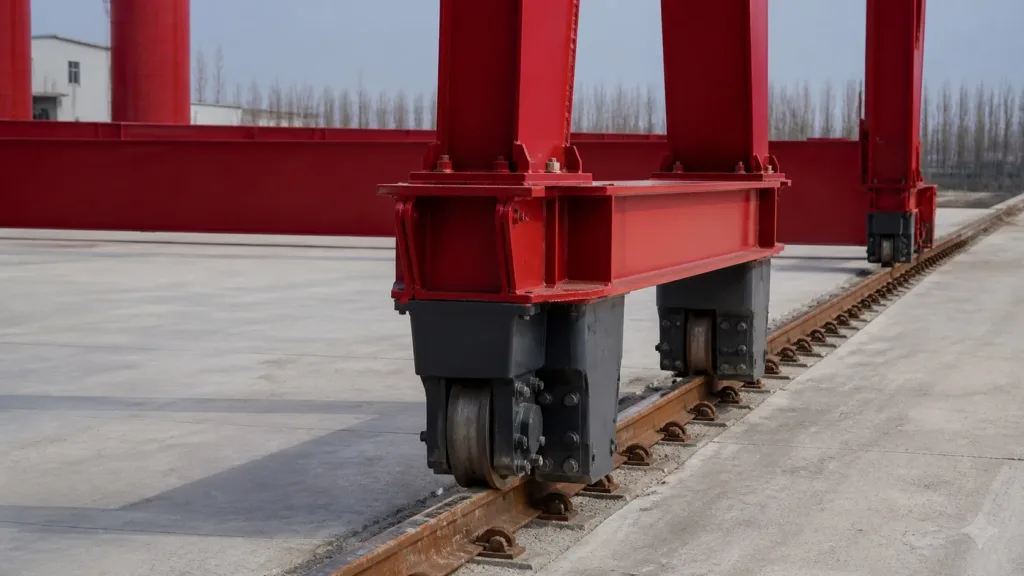
Translate production demand into operating and recovery evidence. 02Which cycle, queue or failure would stop the surrounding process?
Operating sequence, starts, utilisation, dwell, standby, maintenance windows and tolerated recovery time establish the duty, availability and redundancy basis.
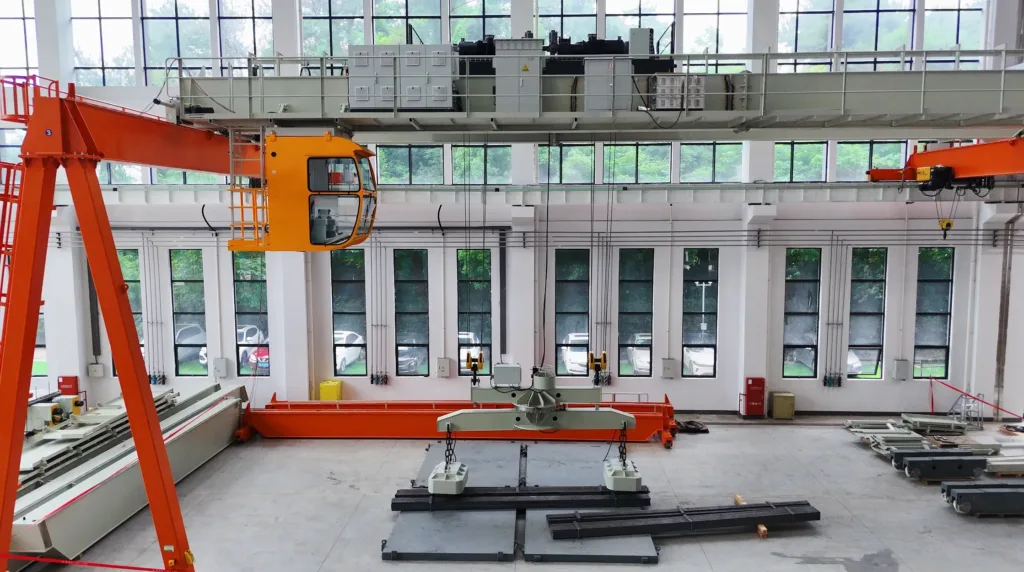
Agree the operating boundary and proof before production. 03How will the crane interact, fail safely and prove the agreed functions?
Operator modes, process signals, interlocks, manual recovery, protection functions, inspection, testing and site acceptance close the system around the real process.
Questions buyers ask.
Before specifying.
These questions usually decide the crane family, project boundary, cost basis and delivery evidence before two process-crane proposals can be compared fairly.
01Which crane family is right for our process?
Start with the material and the job, not a catalogue name. Molten or forged loads point to metals and foundry systems; slabs, coils and plate to metal-stock handling; waste, biomass and loose material to bulk-process cranes; rolls or woodyard duties to paper and forest systems; machine service and repeatable hand-offs to production-integrated cranes; turbines, generators and gates to energy and critical-maintenance systems. If one route crosses several duties, we define the primary system and its interfaces before selecting equipment.
02Can you review a project before the layout or specification is complete?
Yes. An initial review can begin with the load, pick and release points, intended cycle, available building information, photographs or a sketch, destination country and operating environment. Unknown values remain open items; we identify which missing inputs affect the product family, structure, controls, price basis or acceptance plan before a firm proposal.
03Can we reuse our existing runway, building or crane?
Possibly, but reuse must be verified rather than assumed. We review runway and rail geometry, wheel loads, clearances, access, power supply, duty history, controls, equipment condition and the new process demand. The result may be a retained structure with new equipment, a modernisation scope, local strengthening or a completely new system.
04How much automation and redundancy do we actually need?
The answer depends on cycle demand, staffing, positioning accuracy, exposure, upstream and downstream interfaces, maintenance windows and the consequence of a stopped crane. Manual, semi-automatic and unmanned operation are compared together with degraded modes, local control, rescue or recovery moves, spare strategy and the evidence required to prove the agreed availability.
05Can one crane combine special protection and certification requirements?
Yes, when the requirements are compatible and defined at project level. The destination, governing crane standard, hazardous-zone classification, temperature, cleanliness or insulation boundary, required redundancy and component certificates must be reviewed as one configuration. Certification is then tied to the documented equipment and supplied scope—not treated as a generic claim for every crane.
Send the process.
We map the crane.
A process sketch, load states, pick and release points, intended cycle, site information and the consequence of a stopped crane are enough to begin. The first review identifies the credible product family, cross-product requirements and missing acceptance evidence.
Map the process requirement- Mass, temperature, geometry, stability and engagement
- Pick, release, hand-offs, queues and machine states
- Cycles, utilisation, standby and tolerated recovery
- Heat, dust, zone, cleanliness and electrical boundary
- Modes, interlocks, degraded operation and rescue moves
- Building, host systems, destination and proof plan